Aluminium Extrusion Dies
Optimizing high-chromium hot-work tool steels to withstand extreme frictional heat, abrasive wear, and soldering during high-speed aluminium extrusion.
The Challenge and Solutions
In aluminium extrusion, dies face rigorous conditions: the high-speed flow of molten or semi-solid aluminium generates intense frictional heat and abrasive wear at the bearing surfaces. Without proper surface treatment, aluminium tends to "solder" (stick) to the die, causing profile defects, surface tearing, and frequent, costly downtime for die cleaning and correction.
Shital Plasma Nitriding provides a highly controlled, diffusion-based hardening process that modifies the steel surface at a molecular level, offering a distinct advantage over conventional gas nitriding.
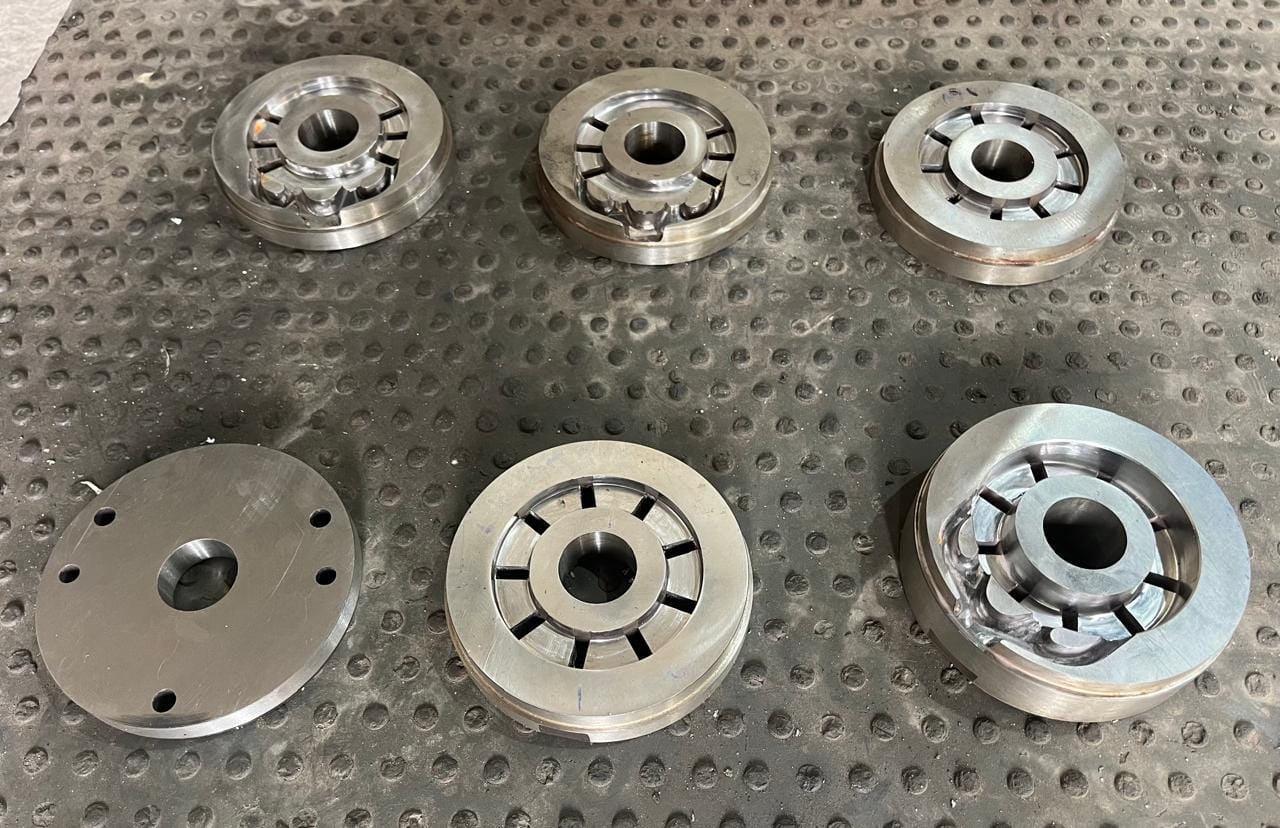
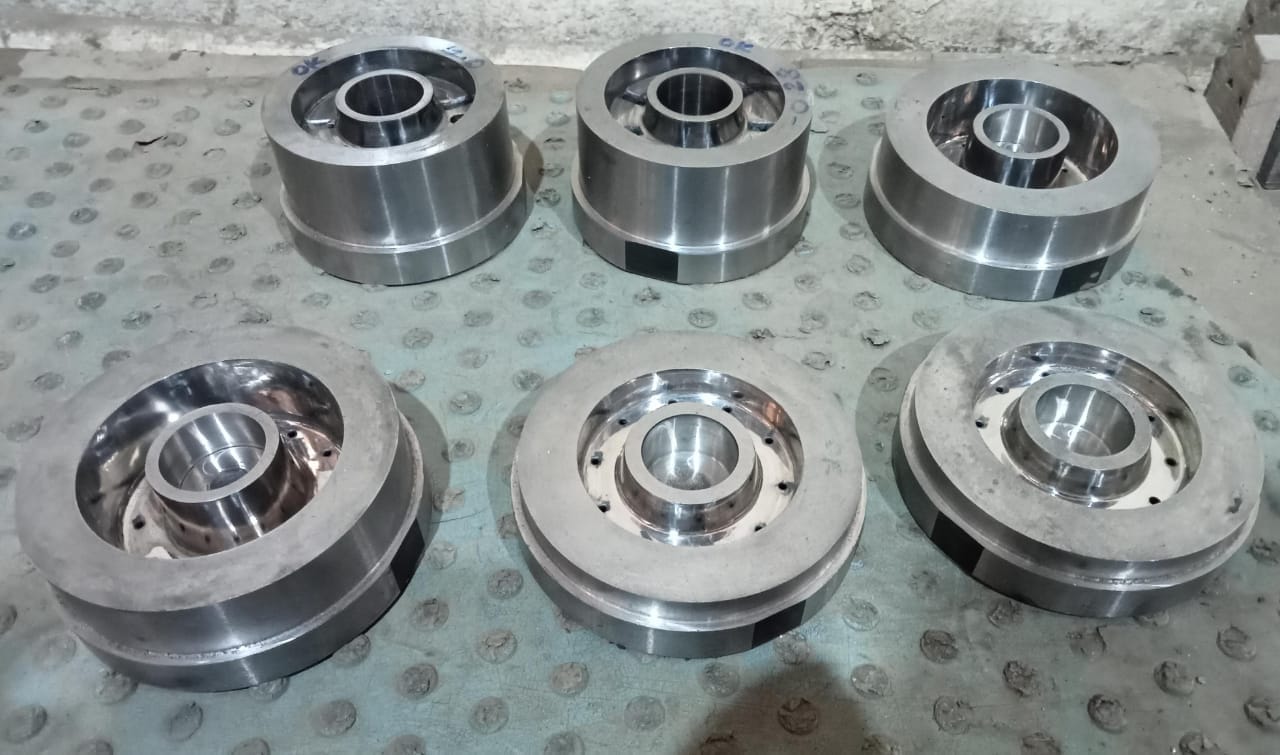
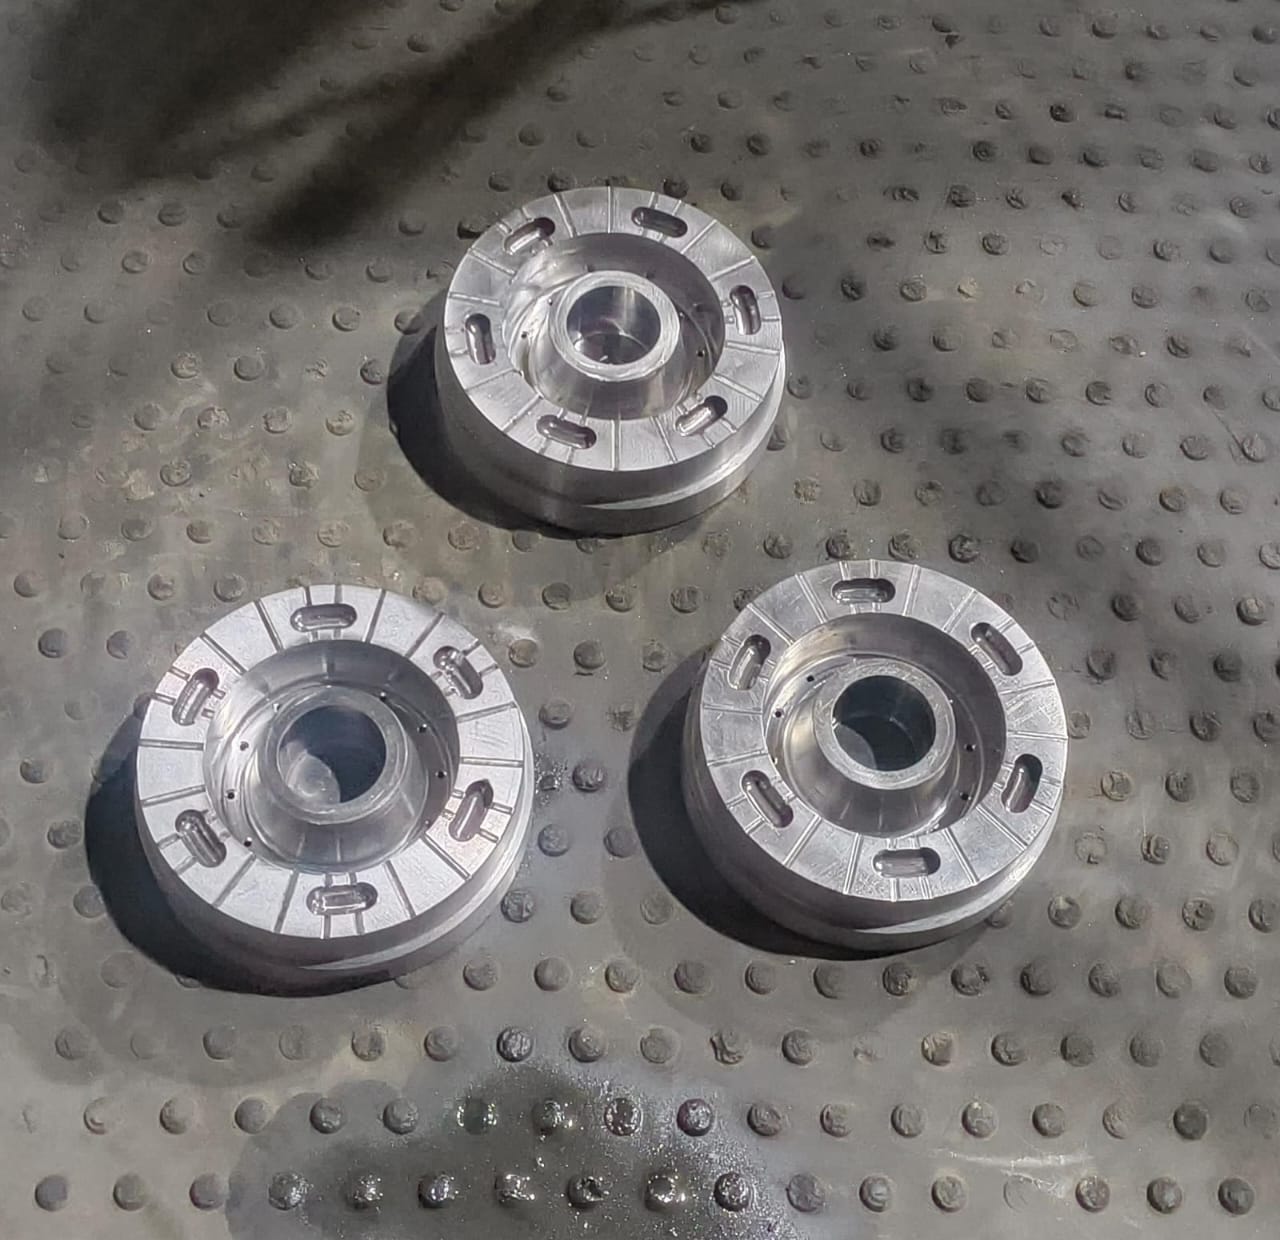
Technical Mitigation of Tooling Failures
| Problem Faced | Mechanism of Plasma Nitriding Solution |
|---|---|
| Sticking of Cast Material | Forms a chemically stable, non-adhesive surface layer that significantly reduces the affinity of aluminium to weld to the steel bearing surface. |
| Heat Check Marks | Increases surface fatigue strength, preventing the initiation of micro-cracks during the repetitive thermal cycling inherent in high-speed extrusion. |
| Surface Erosion | Creates an ultra-hard, wear-resistant diffusion zone that withstands the high-velocity abrasive scouring of aluminium alloys. |
| Thermal Cracking | Enhances structural integrity under high-temperature conditions, preventing premature failure caused by the combined effects of pressure and heat. |
| Wear & Tear | Significantly boosts bearing surface hardness to resist mechanical abrasion from alloy constituents and inclusions during long production runs. |
| Corrosion of Dies | Provides a dense, homogeneous nitride layer that resists chemical attack from aggressive alloy elements and cleaning agents. |
Material Specifications for Aluminium Extrusion Dies
Aluminium extrusion dies are typically manufactured from high-chromium hot-work tool steels. The following specifications are industry-standard targets for optimizing extrusion tool life.
| Material / Grade | Application Area | Target Surface Hardness | Recommended Case Depth |
|---|---|---|---|
| H13 (1.2344) | Die Bearings & Mandrels | 1000 – 1150 HV | 0.10 – 0.25 mm |
| H11 (1.2343) | High-Toughness Dies | 1000 – 1150 HV | 0.10 – 0.25 mm |
| DIN 1.2714 | Heavy-Duty Extrusion Dies | 950 – 1100 HV | 0.15 – 0.30 mm |
| P20+Ni (1.2738) | Bolsters & Support Tooling | 850 – 950 HV | 0.20 – 0.40 mm |