Plastic Moulding Dies
Creating highly smooth, low-friction, and wear-resistant diffusion layers to prevent polymer adhesion, combat abrasive fillers, and protect precision parting lines.
The Challenge and Solutions
In plastic injection moulding, your tooling faces constant exposure to abrasive polymer fillers (like glass fiber), corrosive gases released during resin melting, and the need for precision parting lines. Over time, these factors lead to mold degradation, resulting in costly part defects and increased cycle times due to sticking.
Shital Plasma Nitriding modifies the tool steel surface to provide a superior, low-friction, and hardened barrier that protects your mold integrity and ensures efficient part ejection.
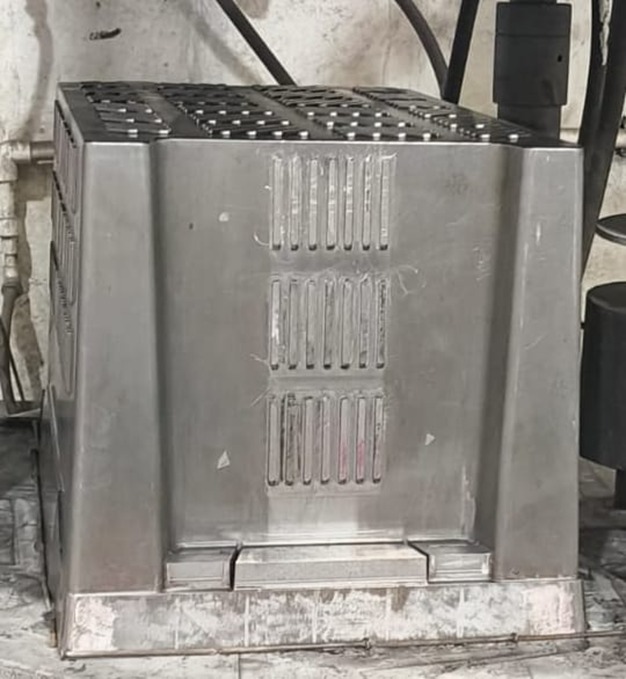
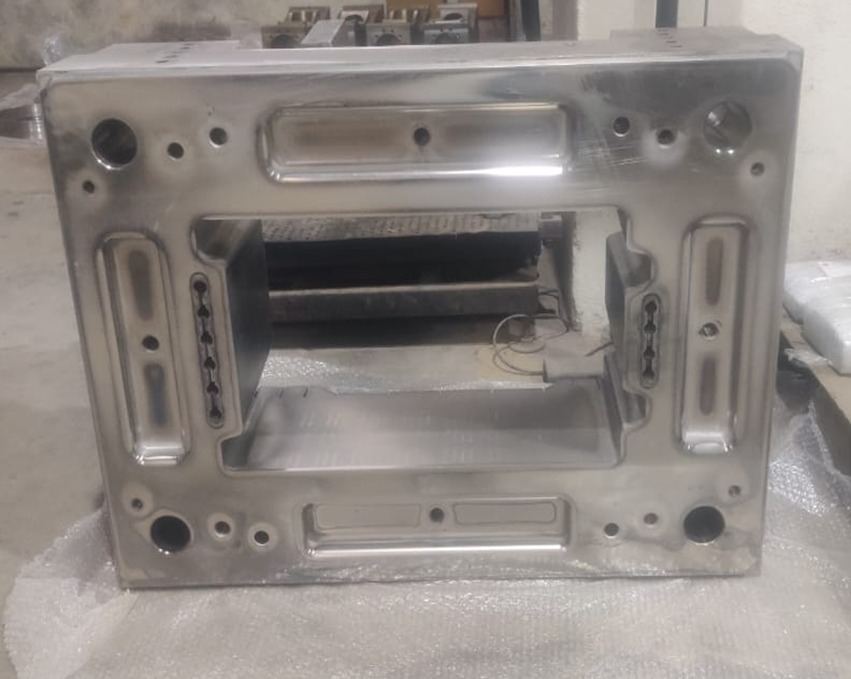
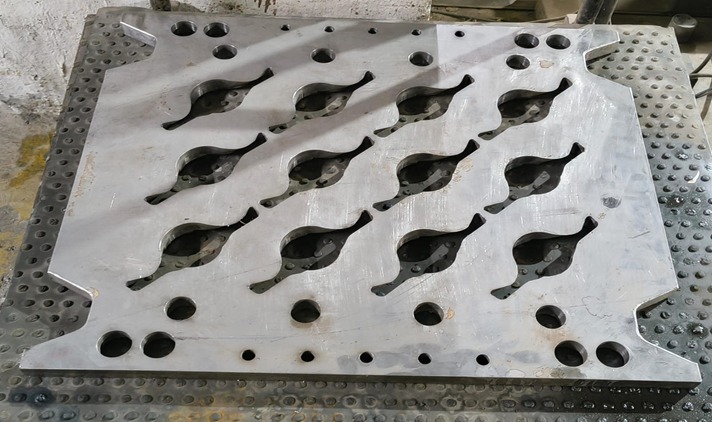
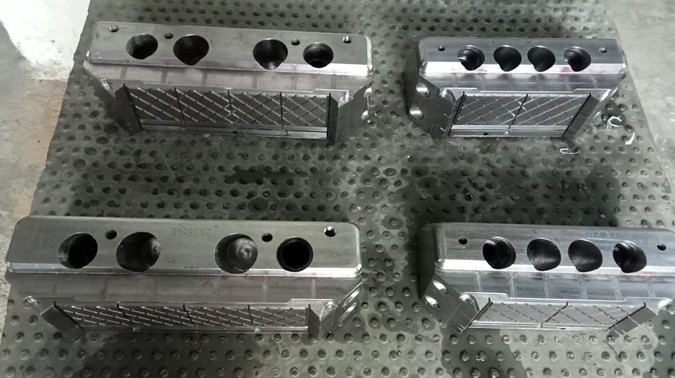
How We Solve Your Plastic Moulding Challenges
| Problem Faced | Mechanism of Plasma Nitriding Solution |
|---|---|
| Sticking of Plastic | Creates a highly smooth, low-surface-energy diffusion zone that reduces the adhesion of molten polymers, ensuring reliable part release. |
| Flash Groove | Increases the surface hardness of shut-off areas, preventing the "peening" or deformation that leads to plastic flash and dimensional inaccuracies. |
| Abrasion | Hardens the cavity and core surfaces to withstand the scouring effect of abrasive materials, such as glass-filled or mineral-filled plastics. |
| Anti Carbon Layer | Inhibits the accumulation of burnt polymer residues and gas deposits, keeping the mold surface clean and maintaining aesthetic surface finishes. |
| Corrosion of Dies | Creates a robust barrier against acidic gases (such as HCl released by PVC or other flame-retardant resins) that typically cause pitting and degradation. |
Material Specifications for Plastic Moulding
Plastic moulding uses a wide range of tool steels. Plasma nitriding is highly effective at boosting the performance of these materials, particularly for long-run production or when processing abrasive/corrosive engineering resins.
| Material / Grade | Application Area | Target Surface Hardness | Recommended Case Depth |
|---|---|---|---|
| P20 (1.2311 / 1.2312) | Mould Bases & Cavities | 750 – 900 HV | 0.20 – 0.35 mm |
| H13 (1.2344) | High-Wear Cavity Inserts | 950 – 1100 HV | 0.15 – 0.25 mm |
| S7 (1.2357) | Slides & Moving Components | 850 – 1000 HV | 0.20 – 0.30 mm |